In the design of metallurgical joints, the strength of the joining material (for example, weld metal) and the adjacent parent material must be considered. The joint should be analyzed on the basis of its loading, the specified allowable strengths, dimensions and geometry.
8.2.1
INTRODUCTION AND DEFINITIONS — The allowable strength for both the adjacent parent metal and the weld metal is given below in the particular section dealing with the method of forming used, and the material being joined. The following subparagraphs define certain joining processes.
Welding — Welding consists of joining two or more pieces of metal by applying heat, pressure or both, with or without filler material, to produce a localized union through fusion or recrystallization across the joint interface. Examples of common welding processes include: fusion [inert-gas, shielded-arc welding with tungsten electrode (TIG) and inert-gas shielded metal-arc welding using covered electrodes (MIG)], resistance (spot and seam), and flash. Several terms used in describing various sections of a welded joint are illustrated in Figure 8.2.1.
Brazing — Brazing consists of joining metals by the application of heat causing the flow of a thin layer, capillary thickness, of nonferrous filler metal into the space between the pieces. Bonding results from the intimate contact produced by the dissolution of a small amount of base metal in the molten filler metal, without fusion of the base metal.
8.2.2
WELDED JOINTS — The weld metal section of a joint should be analyzed on the basis of its loading, specified allowable strength, dimensions and geometry. The effects of the parent metal are to be accounted for as specified herein.
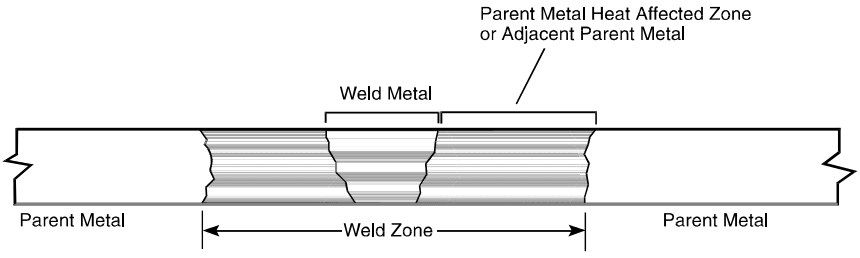
Figure description:
- Weld Zone: The entire central section of the joint, indicated by the horizontal arrow.
- Weld Metal: The central core of the weld joint.
- Parent Metal Heat Affected Zone or Adjacent Parent Metal: The area immediately surrounding the weld metal within the weld zone.
- Parent Metal: The base material on either side of the weld zone.
Figure 8.2.1. Schematic diagram of weld and parent metal.
MIL-HDBK-5J
8.2.2.1
Fusion Welding—Arc and Gas — Section 9.4.2 contains a detailed discussion of one acceptable method of establishing fusion welding allowables. As stated in that section, other methods can be employed as approved by certifying agencies. The following subsections contain specific information for a number of materials.
8.2.2.1.1
Strength of Fusion Welded Joints of Steel Alloys — Allowable fusion weld-metal strengths of steel alloys are shown in Table 8.2.2.1.1(a). Design allowable stresses for the weld metal are based on 85 percent of the respective minimum tensile ultimate test values.
For steel joints welded after heat treatment, the allowable strengths near the weld are given in Tables 8.2.2.1.1(b) and (c).
| Material | Heat Treatment Subsequent to Welding | Welding Rod or Electrode | Fsu ksi | Ftu ksi |
|---|---|---|---|---|
| Carbon and alloy steels | None | AMS 6457 | 32 | 51 |
| AWSA5.1 classes E6010 and E6013 | 32 | 51 | ||
| Alloy steels | None | AMS 6452 | 43 | 72 |
| Alloy steels | Stress relieved | AWSA5.5 class E10013 MIL-E-22200/10, classes MIL- 10018-M1 | 50 | 85 |
| Section Thickness 1/4 inch or less | |
|---|---|
| Type of Joint | Ultimate Tensile Stress, ksi |
| Tapered joints of 30° or lessb | 90 |
| All others | 80 |
| Type of Joint | Bending Modulus of Rupture, ksi |
|---|---|
| Tapered joints of 30° or lessb | Fb from Figure 2.8.1.1 for Ftu = 90 ksi |
| All others | 0.9 of the values of Fb, from Figure 2.8.1.1 for Ftu = 90 ksi |
MIL-HDBK-5J
8.2.2.2
Flash and Pressure Welding — The ultimate tensile allowable strength and bending allowable modulus of rupture for flash and pressure welds are given in Tables 8.2.2.2(a) and (b). A higher efficiency may be permitted in special cases by the applicable procuring or certifying agency upon approval of the manufacturer’s process specification.
8.2.2.3
Spot and Seam Welding — Permission to use spot and seam welding on structural parts is governed by the requirements of the procuring or certifying agency. Table 8.2.2.3 gives the recommended allowable edge distance for spot and seam welds.
8.2.2.3 Recommended Minimum Edge Distance and Spacing for Spot-Welded Jointsᵃ
| Nominal Thicknessb of Thinner Sheet, inch | Minimum Lap Jointc,d Edge Distance, inch | Minimum Spacinge, inch |
|---|---|---|
| 0.016 | 0.19 | 0.19 |
| 0.020 | 0.20 | 0.30 |
| 0.025 | 0.22 | 0.38 |
| 0.032 | 0.25 | 0.46 |
| 0.040 | 0.28 | 0.52 |
| 0.050 | 0.31 | 0.58 |
| 0.063 | 0.38 | 0.67 |
| 0.071 | 0.41 | 0.73 |
| 0.080 | 0.44 | 0.79 |
| 0.090 | 0.47 | 0.89 |
| 0.100 | 0.50 | 1.00 |
| 0.125 | 0.56 | 1.25 |
| 0.160 | 0.69 | 1.60 |
- a Reference Aluminum Association and American Welding Society Handbook.
- b Intermediate gages will require interpolation between adjacent gages.
- c Edge distances are measured materials in contact; this can be to a free edge or to a sheet metal radius where one material bends away from another. Edge distances less than those specified above may be used provided there is no expulsion of weld material or bulging of the edge of the sheet; however, these joints may have less static strength and shorter fatigue life.
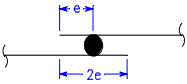
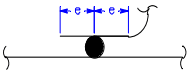
- d Minimum contacting overlap is twice the minimum edge distance.
- e Less than minimum recommended spacing may cause shunting that leads to deterioration of weld strengths and joint life.
MIL-HDBK-5J
8.2.2.3.1
Design Shear Strengths for Spot and Seam Welds in Uncoated Steels and Nickel and Cobalt Alloys — The design shear strength for spot welds for these materials are given in Tables 8.2.2.3.1(a) and (b). The thickness ratio of the thickest sheet to the thinnest outer sheet in the combination should not exceed 4:1.
8.2.2.3.1.1
Effects of Spot-Welds on the Parent Metal Strength of 300 Series Stainless Steel
— In applications of spot welding where ribs, intercostals, or doublers are attached to sheet, either at splices or at other joints on the sheet panels, the allowable ultimate strength of the spot-welded stainless steel sheet will be determined by multiplying the ultimate tensile strength of the sheet (A or S-value) by the appropriate efficiency factors shown in Figures 8.2.2.3.1.1(a) through (c). Efficiencies for gages under 0.012 will be determined by test.
8.2.2.3.2
Design Shear Strengths for Spot and Seam Weldings in Aluminum Alloys — The acceptable aluminum and aluminum alloy combinations for spot and seam welding are given in Table 8.2.2.3.2(a).
Design shear-strength for spot welds in aluminum alloys are given in Tables 8.2.2.3.2(b) and (c). The thickness ratio of the thickest to the thinnest outer sheet in the combination should not exceed 4:1.
Design shear-strength for spot-welded joints, based on tearing of the sheet, is given in Table 8.2.2.3.2(d) for some aluminum alloys, together with the “maximum” pitches that permit attainment of these strengths. Joints having larger pitches fail in the spot welds rather than by tearing of the sheet, and are governed by Tables 8.2.2.3.2(b) and (c). The design shear strengths listed are also applicable to seam welds.
8.2.2.3.2.1
Effects of Spot Welds on Parent Metal Strength of Aluminum Alloys — In applications of spot welding other than splices, where ribs, intercostals, or doublers are attached to sheet, the allowable ultimate strength of the spot-welded sheet may be determined by multiplying the ultimate tensile strength of the sheet (A or S-values) by the appropriate efficiency factor shown on Figure 8.2.2.3.2.1. Efficiencies for gages under 0.020 will be determined by test.
8.2.2.3.2.2
Fatigue Strength of Spot-Welded Joints in Aluminum Alloys — The fatigue strength of spot-welded joints in aluminum alloy are given in Figures 8.2.2.3.2.2(a) through 8.2.2.3.2.2(e).
MIL-HDBK-5J
8.2.2.3.3
Design Shear Strengths for Spot and Seam Welds in Magnesium Alloys — Design shear-strength for spot welds in magnesium alloys are given in Table 8.2.2.3.3. The thickness ratio of the thickest sheet to the thinnest outer sheet in the combination should not exceed 4:1.
8.2.2.3.3 Spot-Weld Design Shear Strength in Panels for Magnesium Alloysᵃ,ᵇ,ᶜ (Welding Specification MIL-W-6858)
| Material Ultimate Tensile Strength, ksi | Design Shear Strength, pounds per spot | |
|---|---|---|
| Greater than 19.5 | Less than 19.5 | |
| Nominal thickness of thinner sheet, in.: | ||
| 0.012 | 24 | 16 |
| 0.016 | 56 | 40 |
| 0.018 | 68 | 52 |
| 0.020 | 80 | 64 |
| 0.022 | 96 | 76 |
| 0.025 | 116 | 88 |
| 0.028 | 140 | 108 |
| 0.032 | 168 | 132 |
| 0.036 | 204 | 156 |
| 0.040 | 240 | 180 |
| 0.045 | 280 | 208 |
| 0.050 | 320 | 236 |
| 0.056 | 380 | 272 |
| 0.063 | 456 | 316 |
| 0.071 | 516 | 360 |
| 0.080 | 612 | 420 |
| 0.090 | 696 | 476 |
| 0.100 | 752 | 540 |
| 0.112 | 800 | 588 |
| 0.125 | 840 | 628 |
- a Strength based on 80 percent of minimum values specified in Specification MIL-W-6858.
- b The allowable tensile strength of spot-welds is 25 percent of the design shear strength. Higher values may be used, however, if these are substantiated by tests acceptable to the procuring or certifying agency.
- c Magnesium alloys AZ31B and HK31A may be spot-welded in any combination.
MIL-HDBK-5J
8.2.2.3.4
Design Shear Strengths for Spot and Seam Welds in Titanium and Titanium Alloys — Design shear strength for spot welds in titanium and titanium alloys are given in Tables 8.2.2.3.4(a) and (b). The thickness ratio of the thickest sheet to the thinnest outer sheet in the combination should not exceed 4:1.
| Tubing | Allowable Ultimate Tensile Stress of Welds |
|---|---|
| Normalized tubing — not heat treated (including normalizing) after welding | 1.0 Ftu (based on Ftu of normalized tubing) |
| Heat-treated tubing welded after heat treatment | 1.0 Ftu (based on Ftu of normalized tubing) |
| Tubing heat treated (including normalizing) after welding. Ftu of unwelded material in heat-treated condition: | |
| < 100 ksi . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . | 0.9 Ftu |
| 100 to 150 ksi | 0.6 Ftu + 30 |
| > 150 ksi | 0.8 Ftu |
| Tubing | Allowable Bending Modulus of Rupture of Welds (Fb from Figure 2.8.1.1 using values of Ftu listed) |
|---|---|
| Normalized tubing — not heat treated (including normalizing after welding | 1.0 Ftu (based on Ftu of normalized tubing) |
| Heat-treated tubing welded after heat treatment. | 1.0 Ftu (based on Ftu of normalized tubing) |
| Tubing heat treated (including normalizing) after welding. Ftu of unwelded material in heat-treated condition: | |
| < 100 ksi .................... | 0.9 Ftu |
| 100 to 150 ksi | 0.6 Ftu + 30 |
| > 150 ksi | 0.8 Ftu |
MIL-HDBK-5J
8.2.3 BRAZING
8.2.3.1
Copper Brazing — The allowable shear strength for copper brazing of steel alloys will be 15 ksi, for all conditions of heat treatment. Higher values may be allowed upon approval of the procuring or certifying agency.
The effect of the brazing process on the strength of the parent or base metal of steel alloys will be considered in the structural design. Where copper furnace brazing is employed, the calculated allowable strength of the base metal which is subjected to the temperatures of the brazing process will be in accordance with the following:
| Material | Allowable Strength |
|---|---|
| Heat-treated material (including normalized) used in “as-brazed” condition | Mechanical properties of normalized material |
| Heat-treated material (including normalized) reheat-treated during or after brazing | Mechanical properties corresponding to heat treatment performed |
8.2.3.2
Silver Brazing — Silver-brazed areas should not be subjected to temperatures exceeding 900°F. Silver brazing alloys are listed in specification QQ-B-654. Deviation from this specification may be allowed upon approval of the procuring or certifying agency.
The allowable shear strength for silver brazing of steel alloys will be 15 ksi, provided that clearances or gaps between parts to be brazed do not exceed 0.010 in. Deviation from this specified allowable value may be allowed upon approval of the procuring or certifying agency.
The effect of silver brazing on the strength of the parent or base metal is the same as shown for copper brazing in Section 8.2.3.1.