The fatigue strength of the standard detail for the normal or shear fatigue stress range, not corrected for effects discussed in 13.2.1, is given below (see also Fig. 22 and Fig. 23):
- b) Shear stres
- a) Normal stress range
when
when
where
- design normal and shear fatigue stress range of the detail, respectively, for life cycle of , and
- normal and shear fatigue strength of the detail for cycles, for the detail category (see Table 26).
Table 26 (a) Detail Category Classification, Group 1 Non-welded Details
(Clauses 13.2.2.1 and 13.3)
| SI No. | Detail Category | Constructional Details | |
|---|---|---|---|
| Illustration (see Note) | Description | ||
| (1) | (2) | (3) | (4) |
| i) | 118 | (1) (2) (3) | Rolled and extruded products i) Plates and flats (1) ii) Rolled sections (2) iii) Seamless tubes (3) Sharp edges, surface and rolling flaws to be removed by grinding in the direction of applied stress. |
| ii) | 103 | (4) (5) (6) | Bolted connections (4) and (5): Stress range calculated on the gross section and on the net section. Unsupported one-sided cover plate connections shall be avoided or the effect of the eccentricity taken into account in calculating stresses Material with gas-cut or sheared edges with no draglines (6): All hardened material and visible signs of edge discontinuities to be removed by machining or grinding in the direction of applied stress. |
| iii) | 92 | (7) | Material with machine gas-cut edges with draglines or manual gas-cut material (7) : Corners and visible signs of edge discontinuities to be removed by grinding in the direction of the applied stress. |
NOTE — The arrow indicates the location and direction of the stresses acting in the basic material for which the stress range is to be calculated on a plane normal to the arrow.
Table 26 (b) Detail Category Classification, Group 2 Welded, Details — Not in Hollow Sections
(Clauses 13.2.2.1 and 13.3)
| SI No. (1) | Detail Category (2) | Constructional Details | |
|---|---|---|---|
| Illustration (see Note) (3) | Description (4) | ||
| i) | 92 | (8) (9) | Welded plate I-section and box girders with continuous longitudinal welds (8) & (9) : Zones of continuous automatic longitudinal fillet or butt welds carried out from both sides and all welds not having un-repaired stop-start positions. |
| ii) | 83 | (10) (11) (12) | Welded plate I-section and box girders with continuous longitudinal welds (10) & (11) : Zones of continuous automatic butt welds made from one side only with a continuous backing bar and all welds not having un-repaired stop-start positions. (12) : Zones of continuous longitudinal fillet or butt welds carried out from both sides but containing stop-start positions. For continuous manual longitudinal fillet or butt welds carried out from both sides, use Detail Category 92. |
| iii) | 66 | (13) | Welded plate I-section and box girders with continuous longitudinal welds (13) : Zones of continuous longitudinal welds carried out from one side only, with or without stop-start positions. |
| iv) | 59 | (14) | Intermittent longitudinal welds (14) : Zones of intermittent longitudinal welds |
| v) | 52 | (15) | Intermittent longitudinal welds (15) : Zones containing cope holes in longitudinally welded T-joints. Cope hole not to be filled with weld. |
| vi) | 83 | (16) (17) (18) | Transverse butt welds (complete penetration) Weld run-off tabs to be used, subsequently removed and ends of welds ground flush in the direction of stress. Welds to be made from two sides. (16) : Transverse splices in plates, flats and rolled sections having the weld reinforcement ground flush to plate surface. 100 percent NDT inspection, and weld surface to be free of exposed porosity in the weld metal. (17) : Plate girders welded as in (16) before assembly. (18) : Transverse splices as in (16) with reduced or tapered transition with taper ≤1:4 |
| Sl No. | Detail Category | Constructional Details | |
|---|---|---|---|
| Illustration (see Note) | Description | ||
| (1) | (2) | (3) | (4) |
| vii) | 66 | (19) (20) TAPER 1:4 (21) | Transverse butt welds (complete penetration) Welds run-off tabs to be used, subsequently removed and ends of welds ground flush in the direction of stress. Welds to be made from two sides. (19) : Transverse splices of plates, rolled sections or plate girders. (20) : Transverse splice of rolled sections or welded plate girders, without cope hole. With cope hole use Detail Category 52, as in (15). (21) : Transverse splices in plates or flats being tapered in width or in thickness where the taper is ≤1:4. |
| viii) | 59 | 1:4 < TAPER ≤ 1:2.5 (22) | Transverse butt welds (complete penetration) Weld run-off tabs to be used, subsequently removed and ends of welds ground flush in the direction of stress. Welds to be made from two sides. (22) : Transverse splices as in (21) with taper in width or thickness >1:4 but ≤1:2.5. |
| ix) | 52 | (23) (24) ≥10 mm | Transverse butt welds (complete penetration) (23) : Transverse butt-welded splices made on a backing bar. The end of the fillet weld of the backing strip shall stop short by more than 10 mm from the edges of the stressed plate. (24) : Transverse butt welds as per (23) with taper on width or thickness <1:2.5. |
| x) | 37 | (25) ≤10 mm | Transverse butt welds (complete penetration) (25) : Transverse butt welds as in (23) where fillet welds end closer than 10 mm to plate edge. |
| xi) | 52 | (26) | Cruciform joints with load-carrying welds (26) : Full penetration welds with intermediate plate NDT inspected and free of defects. Maximum misalignment of plates either side of joint to be <0.15 times the thickness of intermediate plate. |
| xii) | 41 (27) | (27) & (28) | (27) : Partial penetration or fillet welds with stress range calculated on plate area. |
| 27 (28) | (28) : Partial penetration or fillet welds with stress range calculated on throat area of weld. | ||
| xiii) | 46 | (29) TAPER ≤1:2 STRESS AREA OF MAIN PLATE | Overlapped welded joints (29) : Fillet welded lap joint, with welds and overlapping elements having a design capacity greater than the main plate. Stress in the main plate to be calculated on the basis of area shown in the illustration. |
| SI No. (1) | Detail Category (2) | Constructional Details | ||||
|---|---|---|---|---|---|---|
| Illustration (see Note) (3) | Description (4) | |||||
| xiv) | 41 | (30) | [Image for (30) & (31)] (30) & (31) | Overlapped weld joints (30): Fillet welded lap joint, with welds and main plate both having a design capacity greater than the overlapping elements. | ||
| xv) | 33 | (31) | (31): Fillet welded lap joint, with main plate and overlapping elements both having a design capacity greater than the weld. | |||
| xvi) | 66 | (32) | (33) | [Image for (32) and (33)] (32) (33) | Welded attachments (non-load carrying welds)— Longitudinal welds (32): Longitudinal fillet welds. Class of detail varies according to the length of the attachment weld as noted. (33): Gusset welded to the edge of a plate or beam flange. Smooth transition radius (r), formed by machining or flame cutting plus grinding. Class of detail varies according to r/b ratio as noted. | |
| 1/3 ≤ r/b | ||||||
| 59 | l ≤ 50 mm | |||||
| 52 | 50 < l ≤ 100 mm | 1/6 ≤ r/b < 1/3 | ||||
| 37 | 100 mm < l | |||||
| 33 | r/b < 1/6 | |||||
| xvii) | 59 | [Image for (34)] (34) | Welded attachments (34): Shear connectors on base material (failure in base material). | |||
| xviii) | 59 | t ≤ 12 mm | [Image for (35)] | (35) | Transverse welds (35): Transverse fillet welds with the end of the weld ≥10 mm from the edge of the plate. | |
| 52 | t > 12 mm | [Image for (36)] | (36) | (36): Vertical stiffeners welded to a beam or plate girder flange or web by continuous or intermittent welds. In the case of webs carrying combined bending and shear design actions, the fatigue strength shall be determined using the stress range of the principal stresses. | ||
| [Image for (37)] | (37) | (37): Diaphragms of box girders welded to the flange or web by continuous or intermittent welds. | ||||
| xix) | 37 | tf or tp ≤ 25 mm | [Image for (38)] (38) | Cover plates in beams and plate girders (38): End zones of single or multiple welded cover plates, with or without a weld across the end. For a reinforcing plate wider than the flange, an end weld is essential. | ||
| 27 | tf or tp > 25 mm | |||||
| xx) | 67 | [Image for (40)] (40) | [Image for (39)] (39) | Welds loaded in shear (39): Fillet welds transmitting shear. Stress range to be calculated on weld throat area. (40): Stud welded shear connectors (failure in the weld) loaded in shear (the shear stress range to be calculated on the nominal section of the stud). | ||
NOTE — The arrow indicates the location and direction of the stresses acting in the basic material for which the stress range is to be calculated on a plane normal to the arrow.
| Sl No. (1) | Detail Category (2) | Constructional Details | |
|---|---|---|---|
| Illustration (see Note) (3) | Description (4) | ||
| i) | 83 | (41) | Bolts in shear (8.8/TB bolting category only) (41) : Shear stress range calculated on the minor diameter area of the bolt (Ac). NOTE — If the shear on the joint is insufficient to cause slip of the joint the shear in the bolt need not be considered in fatigue. |
| ii) | 27 | (42) | Bolts and threaded rods in tension (tensile stress to be calculated on the tensile stress area, As) (42) : Additional forces due to prying effects shall be taken into account. For tensional bolts, the stress range depends on the connection geometry. NOTE — In connections with tensioned bolts, the change in the force in the bolts is often less than the applied force, but this effect is dependent on the geometry of the connection. It is not normally required that any allowance for fatigue be made in calculating the required number of bolts in such connections. |
NOTE — The arrow indicates the location and direction of the stresses acting in the basic material for which the stress range is to be calculated on a plane normal to the arrow.
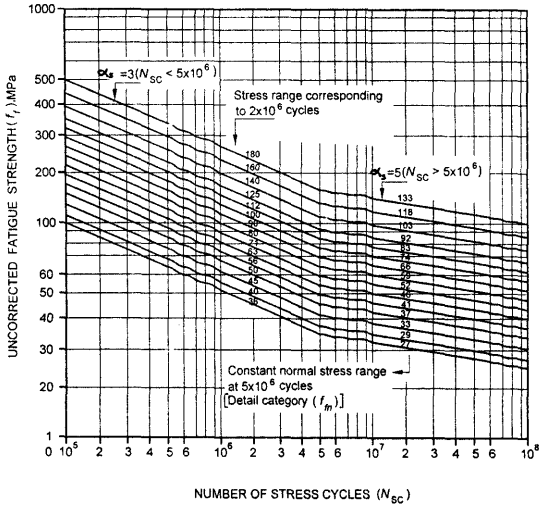
Figure description:
UNCORRECTED FATIGUE STRENGTH (fr, MPa
Uncorrected Fatigue Strength vs. Number of Stress Cycles
Legend
- Fatigue curves for various detail categories (frn — color: black; symbol: solid lines
Annotations
- ms = 3 (Nsc < 5x10^6 (text_label - position: Top-left area where slope is 3))
- ms = 5 (Nsc > 5x10^6 (text_label - position: Right area where slope is 5))
- Stress range corresponding to 2x10^6 cycles (text_label - position: Pointer to labels 180 to 36 at Nsc = 2x10^6)
- Constant normal stress range at 5x10^6 cycles [Detail category (frn (text_label - position: Pointer to the transition point at Nsc = 5x10^6))
| Number of Stress Cycles (Nsc) | fr (MPa for frn=180) | fr (MPa for frn=160) | fr (MPa for frn=140) | fr (MPa for frn=125) | fr (MPa for frn=112) | fr (MPa for frn=100) | fr (MPa for frn=90) | fr (MPa for frn=80) | fr (MPa for frn=71) | fr (MPa for frn=63) | fr (MPa for frn=56) | fr (MPa for frn=50) | fr (MPa for frn=45) | fr (MPa for frn=40) | fr (MPa for frn=36) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1.0E+05 | 488.6 | 434.3 | 380.0 | 339.3 | 304.0 | 271.4 | 244.3 | 217.2 | 192.7 | 171.0 | 152.0 | 135.7 | 122.1 | 108.6 | 97.7 |
| 2.0E+05 | 387.8 | 344.7 | 301.6 | 269.3 | 241.3 | 215.4 | 193.9 | 172.4 | 153.0 | 135.7 | 120.6 | 107.7 | 97.0 | 86.2 | 77.6 |
| 5.0E+05 | 285.7 | 254.0 | 222.2 | 198.4 | 177.8 | 158.7 | 142.9 | 127.0 | 112.7 | 100.0 | 88.9 | 79.4 | 71.4 | 63.5 | 57.1 |
| 1.0E+06 | 226.8 | 201.6 | 176.4 | 157.5 | 141.1 | 126.0 | 113.4 | 100.8 | 89.5 | 79.4 | 70.6 | 63.0 | 56.7 | 50.4 | 45.4 |
| 2.0E+06 | 180.0 | 160.0 | 140.0 | 125.0 | 112.0 | 100.0 | 90.0 | 80.0 | 71.0 | 63.0 | 56.0 | 50.0 | 45.0 | 40.0 | 36.0 |
| 5.0E+06 | 132.6 | 117.9 | 103.1 | 92.1 | 82.5 | 73.7 | 66.3 | 58.9 | 52.3 | 46.4 | 41.3 | 36.8 | 33.2 | 29.5 | 26.5 |
| 1.0E+07 | 115.5 | 102.6 | 89.8 | 80.2 | 71.8 | 64.1 | 57.7 | 51.3 | 45.5 | 40.4 | 35.9 | 32.1 | 28.9 | 25.6 | 23.1 |
| 2.0E+07 | 100.5 | 89.3 | 78.2 | 69.8 | 62.5 | 55.8 | 50.3 | 44.7 | 39.6 | 35.2 | 31.3 | 27.9 | 25.1 | 22.3 | 20.1 |
| 5.0E+07 | 83.7 | 74.4 | 65.1 | 58.1 | 52.1 | 46.5 | 41.9 | 37.2 | 33.0 | 29.3 | 26.0 | 23.2 | 20.9 | 18.6 | 16.7 |
| 1.0E+08 | 72.9 | 64.8 | 56.7 | 50.6 | 45.4 | 40.5 | 36.5 | 32.4 | 28.7 | 25.5 | 22.7 | 20.2 | 18.2 | 16.2 | 14.6 |
Notes: The chart illustrates fatigue strength curves as a function of stress cycles on a log-log scale. The detail category (frn represents the fatigue strength at 2 million cycles. The slope of the curves changes from m=3 to m=5 at 5 million cycles. The rightmost labels (133 to 27 represent the fatigue strength at the 5 million cycle transition point.))
FIG. 22 S-N CURVE FOR NORMAL STRESS
Table 26 (d) Detail Category Classification, Group 4
Welded Details in Hollow Sections
(Clause 13.2.2.1 and 13.3)
| Sl No. (1) | Detail Category (2) | Constructional Details | |
|---|---|---|---|
| Illustration (see Note) (3) | Description (4) | ||
| i) | 103 | (43) | Continuous automatic longitudinal welds (43) : No stop-starts, or as manufactured, proven free to detachable discontinuities. |
| ii) | 66 (t ≥ 8 mm) | (44) | Transverse butt welds (44) : Butt-welded end-to-end connection of circular hollow sections. NOTE — Height of the weld reinforcement less than 10 percent of weld with smooth transition to the plate surface. Welds made in flat position and proven free to detachable discontinuities. |
| 52 (t < 8 mm) | |||
| iii) | 52 (t ≥ 8 mm) | (45) | (45) : Butt-welded end-to-end connection of rectangular hollow sections |
| 41 (t < 8 mm) | |||
| iv) | 41 (t ≥ 8 mm) | (46) | Butt welds to intermediate plate (46) : Circular hollow sections, end-to-end butt-welded with an intermediate plate. |
| 37 (t < 8 mm) | |||
| v) | 37 (t ≥ 8 mm) | (47) | (47) : Rectangular hollow sections, end-to-end butt welded with an intermediate plate. |
| 30 (t < 8 mm) | |||
| vi) | 52 | SECTION WIDTH ≤ 100 mm (48) | Welded attachments (non-load-carrying) (48) : Circular or rectangular hollow section, fillet welded to another section. Section width parallel to stress direction ≤100 mm. |
| vii) | 33 (t ≥ 8 mm) | (49) | Fillet welds to intermediate plate (49) : Circular hollow sections, end-to-end fillet welded with an intermediate plate. |
| 29 (t < 8 mm) | |||
| viii) | 29 (t ≥ 8 mm) | (50) | (50) : Rectangular hollow sections, end-to-end fillet welded with an intermediate plate. |
| 27 (t < 8 mm) | |||
NOTE — The arrow indicates the location and direction of the stresses acting in the basic material for which the stress range is to be calculated on a plane normal to the arrow.